CDMO Services
Pharmaceutical Manufacturing Capabilities at Antique Healthcare
A GMP certified pharma manufacturing facility in India, built on validated pharma production infrastructure and drug manufacturing capabilities that scale with our clients.
Overview
Advanced Pharmaceutical Manufacturing Infrastructure
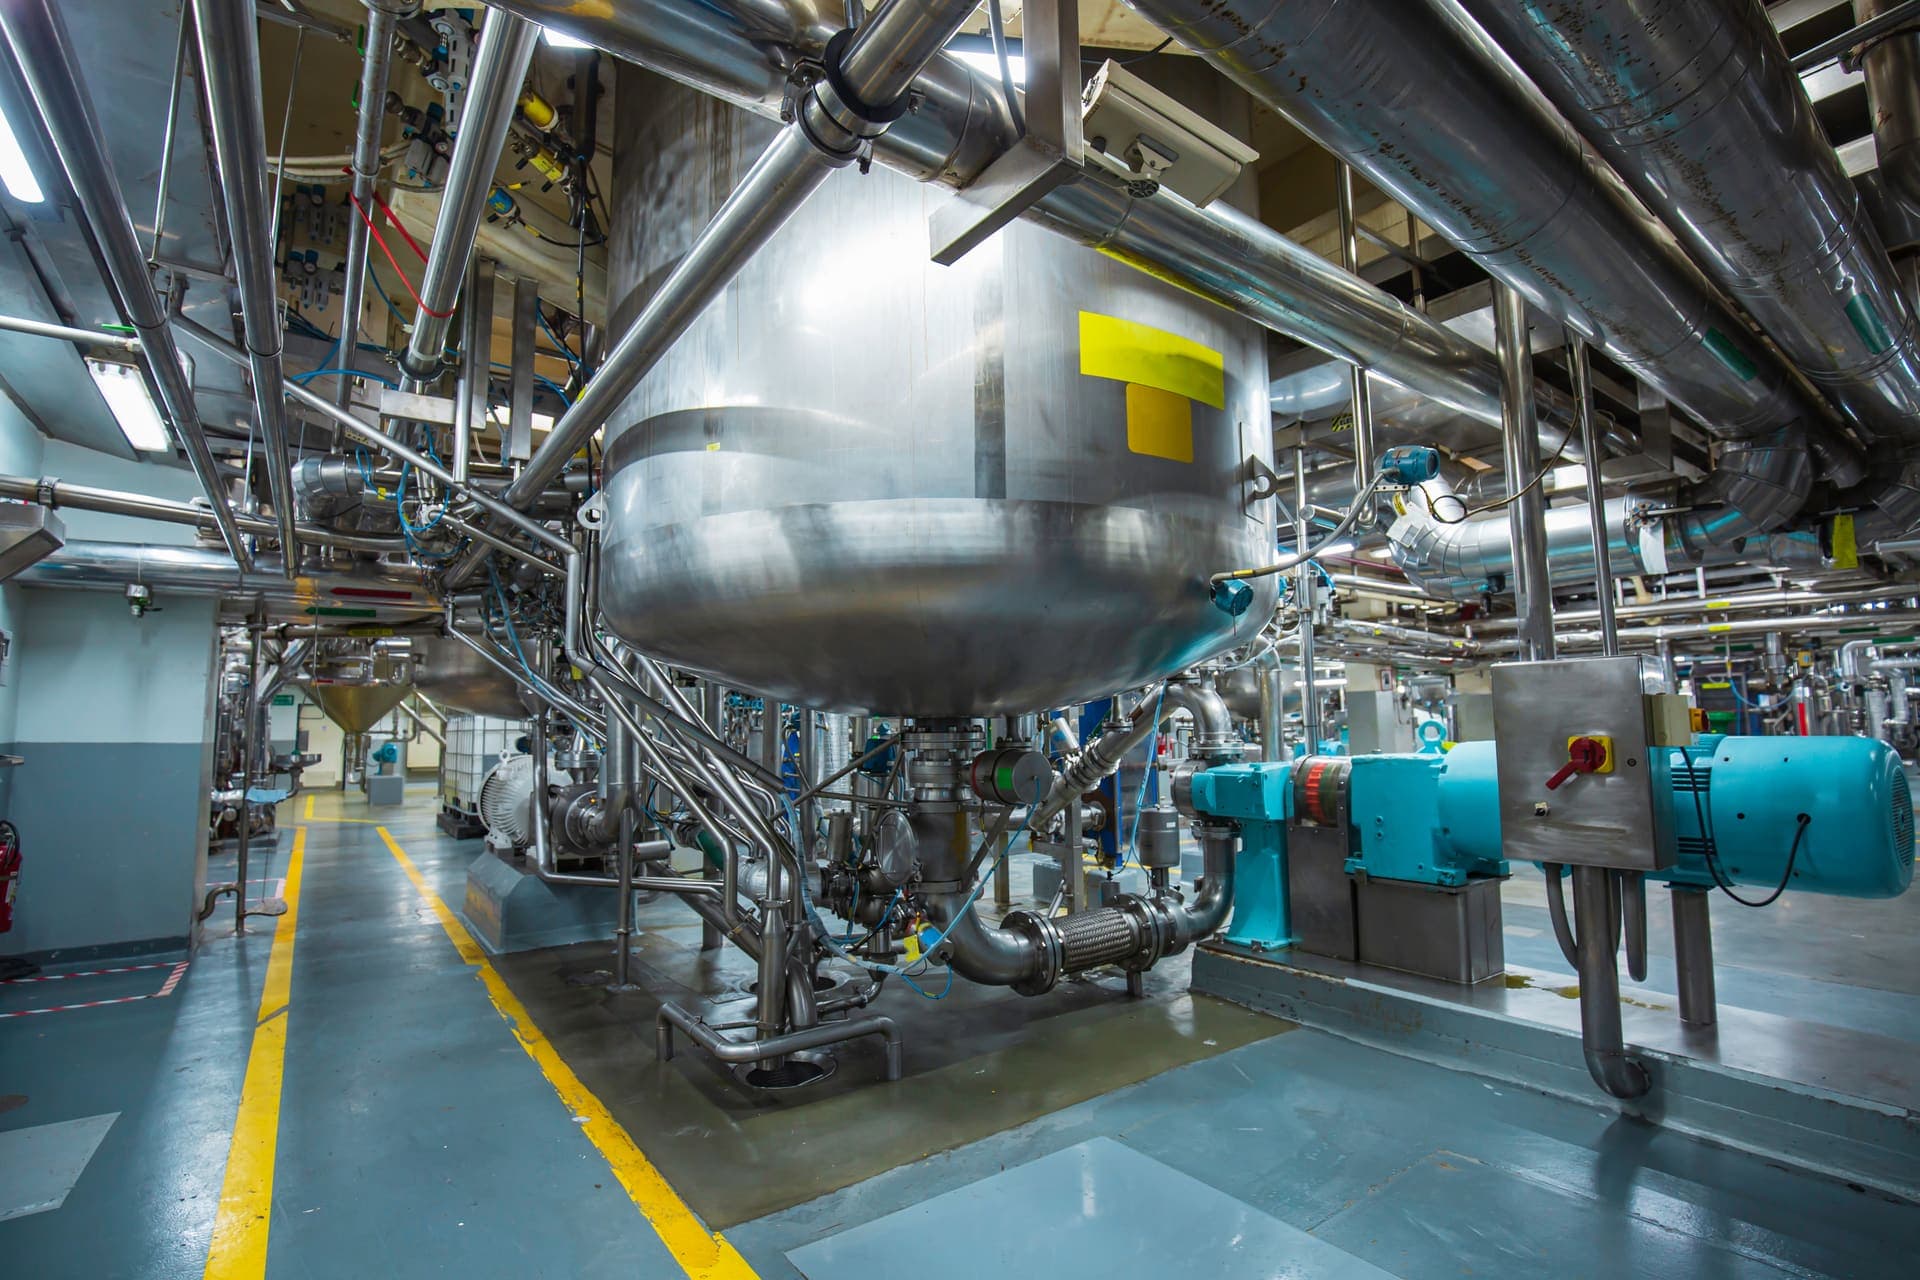
Antique Healthcare functions with strong pharmaceutical manufacturing facilities to cater to the strict demands of the international pharmaceutical sector. Our facilities, processes, and systems are developed to provide quality and scalability to pharmaceutical companies in the global market. Being a pharmaceutical manufacturing company in India, we have developed strong infrastructure and processes to ensure efficiency in our manufacturing operations.
GMP compliance
GMP Certified Pharmaceutical Manufacturing Facility
Our manufacturing process is carried out in a GMP-certified pharmaceutical manufacturing facility. This ensures that our activities are in compliance with Good Manufacturing Practices. Good Manufacturing Practices are the cornerstone of our manufacturing philosophy and ensure that our products are consistently manufactured and controlled according to quality standards.
Good Manufacturing Practices, as followed by Antique Healthcare, include:
These practices ensure that we are always audit-ready and in compliance with regulations.
Infrastructure
Manufacturing Infrastructure Overview
Antique Healthcare's pharmaceutical manufacturing infrastructure is designed to support organized workflows, minimize risk, and maintain consistent product quality.
Production Units
Our production units are designed for efficient process flow and segregation wherever necessary. Each production unit operates in a defined set of manufacturing procedures to ensure consistency in batches and avoid cross-contamination.
The design of the production units concentrates on:
- Material and personnel flow
- Access control and safety provisions
- Effective production planning
- GMP layout requirements
Controlled Manufacturing Environments
Controlled environments are critical in pharmaceutical manufacturing. Antique Healthcare maintains defined environmental conditions such as temperature, humidity, and cleanliness to protect product quality throughout the manufacturing process.
These controls support:
- Product stability and safety
- Compliance with regulatory requirements
- Reduction of contamination risks
Equipment & Manufacturing Technology
Antique Healthcare utilizes validated manufacturing equipment and modern technology to ensure accuracy, efficiency, and repeatability. Equipment qualification and routine maintenance programs ensure consistent performance and compliance.
Our equipment strategy includes:
- Equipment qualification and validation
- Preventive maintenance programs
- Calibration and performance monitoring
- Process optimization through technology
Quality control
Quality Control Laboratories
Quality control is a critical part of our manufacturing capacity. Antique Healthcare has its own quality control laboratories to support in-process testing and finished product testing.
The quality control process includes:
Raw material testing
In-process testing
Finished product testing
Stability testing
The above process ensures that the products meet the predetermined quality specifications.
Quality assurance
Quality Assurance Systems
Quality assurance (QA) oversees compliance, documentation accuracy, and continuous improvement across manufacturing operations. Our QA systems ensure that GMP guidelines are consistently followed and deviations are promptly addressed.
Key QA functions include:
SOP management and documentation control
Deviation and change control
CAPA implementation
Audit preparation and support
Compliance
Regulatory Compliance & Audit Readiness
Antique Healthcare maintains audit-ready systems across all manufacturing operations. Our compliance framework supports internal audits, client audits, and regulatory inspections.
Regulatory compliance activities include:
Documentation management
Audit preparedness programs
Corrective and preventive actions
Continuous compliance monitoring
Our proactive compliance approach reduces regulatory risk and ensures uninterrupted manufacturing operations.
Scalability
Scalable Pharmaceutical Manufacturing Capabilities
Our production facilities are intended to facilitate scalable pharmaceutical manufacturing, enabling clients to scale their businesses without sacrificing quality or regulatory compliance.
The advantages of scalability include the following:
Flexible production scheduling
Effective scale-up procedures
Consistent batch production
Resource optimization
Scalability will benefit both new pharmaceutical firms and established brands with expanding product portfolios.
Integration
Integration With CDMO & Contract Manufacturing Services
Antique Healthcare's manufacturing capabilities are fully integrated with our CDMO services and pharmaceutical contract manufacturing operations. This integration ensures seamless coordination between development, manufacturing, and quality functions.
Integrated operations provide:
Safety
Safety, Sustainability & Operational Excellence
Safety and sustainability are integral to our manufacturing operations. Antique Healthcare implements safety protocols and responsible manufacturing practices to protect personnel, products, and the environment.
Our operational excellence initiatives focus on:
Workplace safety
Efficient resource utilization
Waste minimization
Continuous process improvement
Why us
Why Choose Antique Healthcare for Manufacturing Capabilities
Antique Healthcare offers manufacturing capabilities that combine infrastructure strength with disciplined execution and quality-driven operations.
Why clients choose us:
We work as a reliable manufacturing partner supporting long-term pharmaceutical growth.
Partner With a Capable Pharmaceutical Manufacturer
If you are seeking a pharmaceutical manufacturing partner in India with proven infrastructure, regulatory compliance, and scalability, Antique Healthcare provides the manufacturing capabilities needed to support your business objectives.
Contact our team to discuss your pharmaceutical manufacturing requirements.